Custom Medicine Boxes That Protect Products and Patients
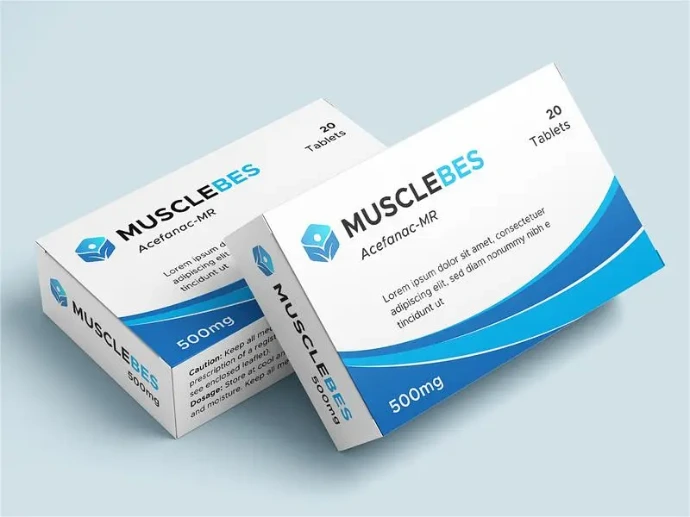
Medicine packaging carries a heavier responsibility than almost any other category. It has to protect a product that people depend on, communicate information that must not be misread, and satisfy regulatory expectations that leave little room for error. Custom Medicine Boxes are a functional part of how a medication works safely, not simply a container for it.
The Visions Packaging is a direct manufacturer of custom packaging boxes in the USA, supplying pharmaceutical companies, generic manufacturers, compounding pharmacies, and OTC brands with medicine packaging built to the standards the category demands.
Engineered Around What Is Inside
Medicine comes in blister packs, bottles, vials, sachets, tubes, and strips, and each format places different demands on a carton.
Blister packs need a box sized so strips sit flat without bending, with enough depth to accommodate a folded patient information leaflet. Bottles need internal clearance so caps are never under pressure and inserts that stop movement and rattle. Vials and ampoules need compartmented protection because glass breakage is a total loss. Tubes need structure that holds its shape around a flexible product.
We manufacture to your exact dimensions rather than fitting your product into an approximate stock size, because in this category an approximate fit is a real quality risk.
Tamper-Evident and Child-Resistant Features
Patient safety starts with knowing a package has not been interfered with. We build tamper-evident features directly into your Custom Medicine Boxes rather than adding them afterwards.
Sealed end flaps, tear-strip openings, perforated closures, and security label positioning all provide visible assurance. Where your product requires child-resistant features, we design structures that accommodate them without making the box impractical for adults with limited dexterity — a genuine consideration for medication aimed at older patients. Serialization and track-and-trace coding areas are built into the layout so batch numbers, expiry dates, and unique identifiers can be applied cleanly in production.
Information Design That Prevents Mistakes
Dosage errors are a serious patient safety problem, and packaging design is part of the cause. Cramped type, poor contrast, and confused hierarchy all contribute.
We take information architecture on medicine packaging seriously. Drug name and strength get unambiguous prominence. Dosage form, quantity, and route of administration follow clearly. Warnings, storage requirements, and expiry information are placed where they will be seen rather than buried. Braille embossing is available where required. If you produce several strengths of the same medication, distinct color-coding across an identical structure meaningfully reduces the risk of a dispensing error.
Materials That Protect Product Integrity
Pharmaceutical-grade paperboard is the standard for medicine cartons, offering a clean, uniform surface and consistent structural performance across production runs.
For products sensitive to light, humidity, or temperature, we offer stock with barrier properties and coatings that add protection. E-flute corrugated is available for shipper cartons and bulk distribution, where cases are stacked and handled through a supply chain. Eco-friendly kraft suits herbal, ayurvedic, and natural remedy products where a non-clinical appearance suits the positioning better.
All materials we use are recyclable, which matters increasingly as healthcare systems and pharmacy chains apply sustainability criteria to their suppliers.
In-House Printing Built for Regulatory Content
Medicine packaging carries dense text that must remain legible at small point sizes — active ingredients, excipients, contraindications, storage instructions, and manufacturer details. There is no room for smudged or inconsistent printing.
Our in-house offset and digital printing delivers the sharpness that requires, with CMYK and PMS color matching that keeps your brand and color-coding identical across every batch. Barcodes, data matrix codes, and QR codes print at scan-reliable quality. Consistency matters enormously here, because pharmacists and patients use color and layout as recognition cues.
Structural Styles for Pharmacy and Distribution
Reverse tuck end and straight tuck end cartons are the standard for retail pharmacy and OTC shelves. Auto-bottom boxes provide a stronger base for heavier bottles and liquid products. Sealed-end cartons offer maximum tamper evidence for prescription products.
Hanging tab boxes suit peg displays in pharmacy and grocery retail. Larger cartons with inserts accommodate kits, courses of treatment, and combination products. Corrugated shipper cases protect retail cartons through distribution. We design the full packaging chain, not just the individual box.
Wholesale Pricing With No Hidden Charges
We manufacture directly, so our pricing reflects production cost without distributor margin. Minimum order is 50 boxes, which makes small-batch, compounded, and specialty products practical to package properly. Unit pricing drops significantly at the volumes pharmaceutical production typically requires.
There are no die charges, no plate charges, and no setup fees. Graphic design is free, shipping across the USA is free, and the quote we issue is the price you pay.
Reliable Turnaround for Supply Chain Planning
Pharmaceutical supply chains do not tolerate surprises. Standard turnaround is 15 to 18 days after final design approval, with a rush service available at 10 to 12 days. Every order includes a free digital proof for approval, and larger orders qualify for free physical samples so you can verify fit and finish before committing to a full run.
Contact The Visions Packaging for a free quote and medicine packaging built to the standard your product requires.